Power plants generate a large amount of maintenance and inspection information every day. Operators complete rounds. Technicians document repairs. Contractors submit reports. Engineers review abnormal conditions. Reliability teams analyze failures. Asset managers track age, condition, criticality, and replacement plans.
The challenge is not always that power generation facilities lack data. The challenge is that much of this information is often reviewed as individual records rather than as part of a long-term asset history.
A pump inspection, valve repair, turbine auxiliary finding, boiler observation, heat exchanger issue, cooling system concern, or electrical maintenance note may appear routine when reviewed alone. When the same type of finding appears repeatedly on the same asset, across similar equipment, or before a larger failure, it may point to a reliability issue that deserves closer attention.
For power plant O&M teams, better inspection history is not about creating more documentation. It is about making existing inspection and maintenance records useful enough to support better maintenance prioritization, outage planning, and asset decisions.
Recurring Equipment Issues Often Look Routine
Many power plant problems do not begin as major failures. They develop gradually through heat, vibration, cycling, corrosion, fouling, contamination, lubrication issues, pressure changes, mechanical wear, or changing operating conditions.
A pump may show repeated seal leakage. A valve may require recurring adjustment. A fan may show vibration findings over several inspection cycles. A heat exchanger may develop repeated fouling or performance concerns. Electrical cabinets may show recurring heat, dust, or moisture-related findings. A boiler auxiliary system may require repeated minor repairs before the pattern receives broader review.
Each individual finding may be addressed properly at the time. The maintenance task is created, work is assigned, the repair is completed, and the record is closed. The problem begins when the same condition returns and the history does not make that recurrence easy to see.
When inspection reports, work orders, photos, contractor notes, test results, and corrective actions are scattered across different systems or folders, teams may only see the latest event. That makes it harder to determine whether a condition is new, recurring, worsening, or connected to previous maintenance.
Inspection Records Need Asset-Level Context
A completed inspection confirms that a task was performed. It does not always give future teams enough information to understand the condition of the asset over time.
A useful inspection record connects each finding to the specific asset, component, location, observed condition, severity, supporting evidence, corrective action, and follow-up result. A note that says “pump repaired” or “valve checked” may close a task, but it does not provide enough detail for future troubleshooting.
A stronger record explains what was found, where it was found, how severe it was, whether the issue had appeared before, what action was taken, and whether the condition returned after the repair.
Digital approaches to inspection data management can help organize inspection findings, asset condition histories, corrective actions, photos, and reports in a more consistent workflow.
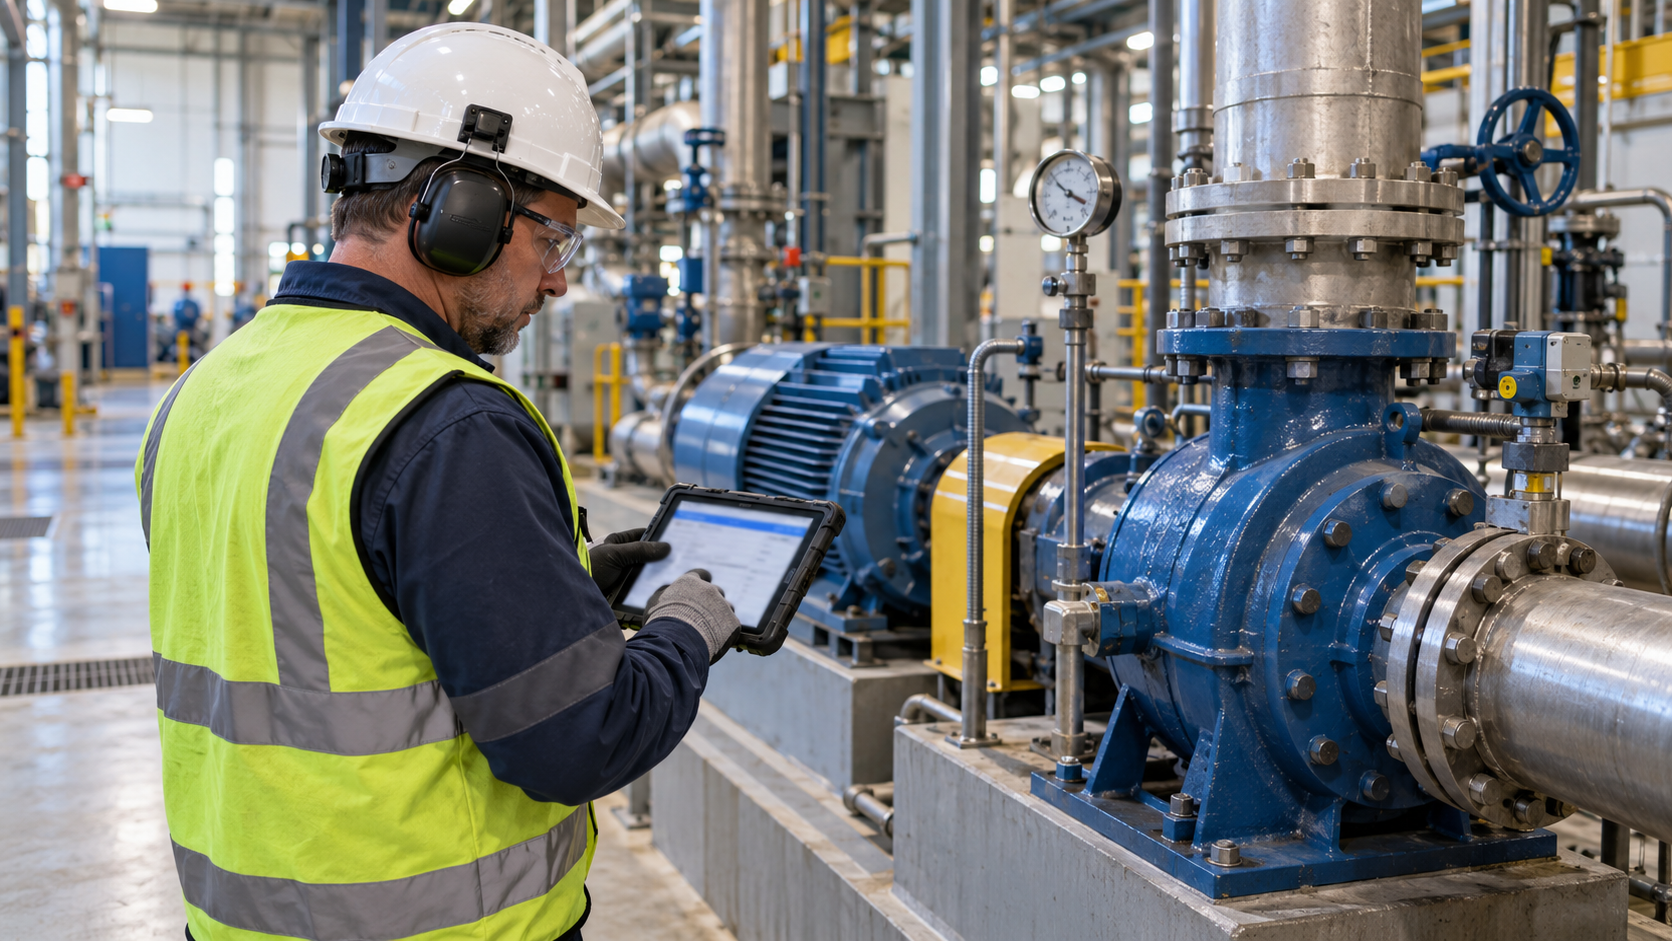
This is especially important in power generation because plants often operate many similar assets across balance-of-plant systems, auxiliary systems, cooling water systems, fuel handling equipment, electrical distribution, emissions control systems, and rotating equipment. One finding on one asset may not be unusual. Repeated findings across similar assets may suggest an issue with operating conditions, design, installation, inspection frequency, maintenance practice, or replacement strategy.
Corrective Actions Should Close the Loop
Corrective-action tracking is one of the most important parts of any inspection and maintenance program. It is also one of the places where useful reliability information can be lost.
A finding is identified, a work order is created, and the repair is completed. The record is marked closed. From an administrative standpoint, the task is complete. From a reliability standpoint, the larger question remains: did the action solve the problem?
For O&M teams, corrective actions should show more than completion status. They should explain what was found, what work was performed, whether parts were replaced, whether testing or verification was completed, whether follow-up inspection is needed, and whether similar conditions have appeared before.
If a pump seal is replaced several times, the history should help determine whether the prior corrective actions addressed the actual cause. If a motor repeatedly shows elevated temperature, the record should help the team review loading, ventilation, alignment, environmental conditions, and previous maintenance actions. If a valve continues to generate similar findings, the team should be able to see whether the issue is related to application, actuation, operating practice, or component selection.
Closing the task is not the same as closing the loop. Maintenance teams gain more value when corrective actions become part of a searchable asset history that can be reviewed over time.
Better History Supports Outage Planning
Outage planning depends on good information. O&M teams must decide what work should be included, what can wait, what requires parts or contractor support, and what needs engineering review before the outage window begins.
Inspection history can help make those decisions more evidence-based. A single inspection finding may not justify adding work to an outage scope. Repeated findings on a critical asset may. A repair that has been completed several times without lasting improvement may need deeper review. A condition that is worsening across inspection cycles may require planned intervention before it creates forced outage risk.
For example, if several inspections show recurring vibration findings on a fan, maintenance planners may decide to include alignment, balancing, bearing inspection, or foundation review during the next planned outage. If heat exchanger performance concerns continue to appear, the team may review cleaning scope, fouling history, water quality, and inspection frequency. If an electrical asset shows recurring heat signatures, the outage plan may need to include testing, torque checks, replacement parts, or engineering review.
The value of inspection history is that it helps teams move from reactive work selection to planned risk-based decision making.
Maintenance Prioritization Requires More Than the Latest Report
Power plant maintenance teams rarely have unlimited time, budget, or labor. They must decide which issues require immediate attention, which can be scheduled, which should wait for an outage, and which require capital planning.
The latest inspection report is important, but it may not be enough. A new minor finding on a noncritical asset may be handled through routine maintenance. The same finding repeated several times on a critical system may deserve escalation. A defect that appears across several similar assets may point to a broader issue. A corrective action that has been completed repeatedly without lasting improvement may require a different approach.
Inspection history helps teams prioritize based on evidence rather than only urgency, memory, or the most recent complaint. This also improves communication among departments. Operations teams need to understand how equipment condition affects availability. Maintenance teams need to know which assets are consuming repeated labor and parts. Reliability teams need visibility into patterns across systems.
Engineering teams need evidence when deciding whether to modify, replace, or redesign equipment. Finance and asset managers need a defensible basis for repair-versus-replace decisions. A shared asset history gives these groups a common factual basis for discussion.
AI Depends on Organized Maintenance Records
Artificial intelligence (AI) is increasingly discussed in maintenance, reliability, and asset management. AI-supported tools may help power plant teams review inspection history, identify recurring defects, compare similar assets, and prioritize maintenance activities.
However, AI cannot create reliable insight from poor records. If asset names are inconsistent, defect categories are vague, photos are not connected to the correct equipment, severity ratings vary widely, and corrective actions do not show outcomes, advanced analytics will have limited value. AI-supported maintenance recommendations are only as useful as the data behind them.
AI can help preventive maintenance programs by analyzing inspection history, asset condition, recurring defects, and corrective-action outcomes to identify risk patterns and support more informed maintenance planning.
For broader AI implementation, the same principle applies. AI is more useful when connected to business workflows, structured data, and specific decision points rather than treated as a standalone model.
For power plants, preparing for AI does not start with a complex model. It starts with disciplined inspection and maintenance records. That means consistent asset identification, clear defect descriptions, complete inspection notes, reliable photos, structured corrective actions, and useful closure information. These practices improve maintenance decisions today and create a stronger foundation for future analytics.
AI should support O&M judgment, not replace it.
Practical Steps For O&M Teams
Power plant teams do not need to rebuild their entire maintenance program to make better use of inspection history. They can start with practical improvements.
First, standardize how findings are recorded. Similar conditions should be described in similar language so they can be compared across assets and time.
Second, connect every finding to the correct asset and component. Inspection records, photos, work orders, test results, and corrective actions should remain tied to the equipment involved.
Third, improve corrective-action closure notes. “Completed” may close a work order, but it does not help future planning. Closure notes should explain what was done, whether the issue was verified, and whether follow-up is needed.
Fourth, review repeat findings regularly. Maintenance, operations, reliability, and engineering teams should look for assets, components, systems, or conditions that continue to generate similar issues.
Fifth, use inspection history during outage planning. Recurring findings can help determine outage scope, spare parts needs, contractor requirements, inspection priorities, and engineering review.
Finally, keep records practical. The goal is not to create unnecessary administrative work. The goal is to make inspection and maintenance records useful to the people who need to operate, maintain, troubleshoot, and manage the plant.
From Maintenance Data to Better Reliability Decisions
Power plants already collect valuable inspection and maintenance information. The opportunity is to make that information easier to use over time.
A single inspection record shows what was observed on one day. A connected inspection history shows whether the condition is new, recurring, worsening, or tied to previous corrective actions. That history helps O&M teams identify patterns, prioritize maintenance, support outage planning, reduce repeat work, and make stronger asset decisions.
For power generation facilities, inspection history is not simply documentation. It is part of how reliability decisions are made. The most valuable record is not the one that proves an inspection was completed. It is the one that helps the next person understand what happened, what was done, and whether the condition is likely to return.
—Palak Sheth, a marketing specialist for Konverge Digital Solutions, writes about inspection management, asset reliability, preventive maintenance, and AI-enabled workflows for industrial operations.